Consistency, accuracy, and speed sit at the heart of pharmaceutical production. Whether filling vials, running blister lines, or finishing sachets, even tiny deviations can affect yield, costs, and compliance-ready documentation. Inline checkweighing has become essential not only for meeting regulatory expectations but also for helping manufacturers work more productively. Today’s systems combine high-performance weighing, intelligent product handling, robust connectivity and clear validation processes, creating more efficient, stable and future-ready operations.
Greater precision, less waste
Productivity depends heavily on accurate weighing, especially with small or high-value formats. FlashCel Electromagnetic Force Restoration (EMFR) load cells support this by achieving accuracy from ±0.01 g. Such precision helps manufacturers minimise overfill, avoid rework, and reduce unnecessary giveaway, which is especially valuable when using costly ingredients. EMFR technology also sustains high line speeds, supporting throughput without compromising weighing integrity. With vibration compensation and air-flow control, results remain consistent even where external influences might otherwise distort readings.
Automated reporting that saves time
Compliance may be mandatory, but the way organisations manage it can have a real impact on efficiency. Pharmaceutical producers need secure electronic records that capture users, weighing events, and process changes. Modern checkweighers support this through audit-ready data structures aligned with recognised expectations on electronic traceability, user management, and security. Automatic communication to enterprise systems replaces manual record gathering and streamlines audits. Instead of searching for historical reports, documentation is already structured, timestamped, and centrally stored. Making accurate weighing data and validation records available on demand allows internal teams to focus on performance and line optimisation rather than administration.
Greater efficiency through tailored product handling
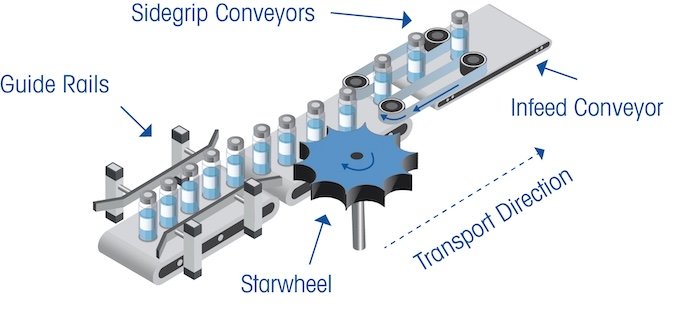
Accurate results depend just as much on product handling as on weighing technology. Many pharmaceutical items are small, lightweight, or delicate; so reliable transfer is essential. A vial that wobbles, a pouch that twists, or a carton that tips can lead to false rejects, avoidable stoppages, or further checks. Handling solutions such as spacing conveyors, timing screws, and side-grip units keep products stable, correctly pitched, and aligned for weighing. Gentle reject mechanisms remove non-conforming items without slowing the line or damaging sensitive formats. These features enable high-speed operation while protecting accuracy, supporting multi-lane layouts where space is tight, and keeping results dependable at pace.
Plug-and-play flexibility for complex lines
Many pharmaceutical sites run well-established filling, cartooning, and packaging operations; so new inspection systems must integrate cleanly without major rework or re-qualification. Modular frames, digital connectivity, and support for OEM alignment mean checkweighers can sit within existing footprints with minimal disruption. Standard communication protocols allow the secure exchange of weighing data, audit records, and machine feedback with ERP or MES platforms. Straightforward integration shortens commissioning, reduces stoppages, and gives manufacturers flexibility to evolve lines or introduce new formats over time. When equipment is easy to connect, validate, and manage, it supports smoother day-to-day performance and longer-term resilience.
Productive from the start
Productivity also relies on how quickly a system becomes validated and fully operational. Equipment Qualification Packs provide structured processes covering installation, testing, operational qualification, documentation, and operator training, helping get new assets into compliant production faster. Clear validation pathways reduce internal workload and give teams more time to concentrate on running stable lines. Over time, preventative maintenance, calibration support, verification checks, and refresher training all help maintain weighing performance, limit disruption, and protect yields. In regulated environments where every hour matters, these service layers support long-term productivity by keeping equipment at expected performance.
Driving productivity through precision, intelligence and partnership
Dynamic checkweighing in pharmaceuticals is no longer simply a pass-or-fail step. It’s a strategic tool that underpins performance across the line. By combining precise EMFR weighing, intelligent handling, automated reporting, seamless integration, and structured qualification, manufacturers can achieve accurate results at speed while scaling performance, strengthening compliance, and building stability for the future. Whether handling delicate vials, complex cartons, or multi-lane requirements, modern checkweighing helps pharmaceutical producers deliver reliable output, reduce waste, and free specialist time where it matters most. In a sector defined by quality, control, and trust, the right checkweighing platform can help organisations not just meet targets but exceed them.